

CATEGORIES
Steel wire calendering line
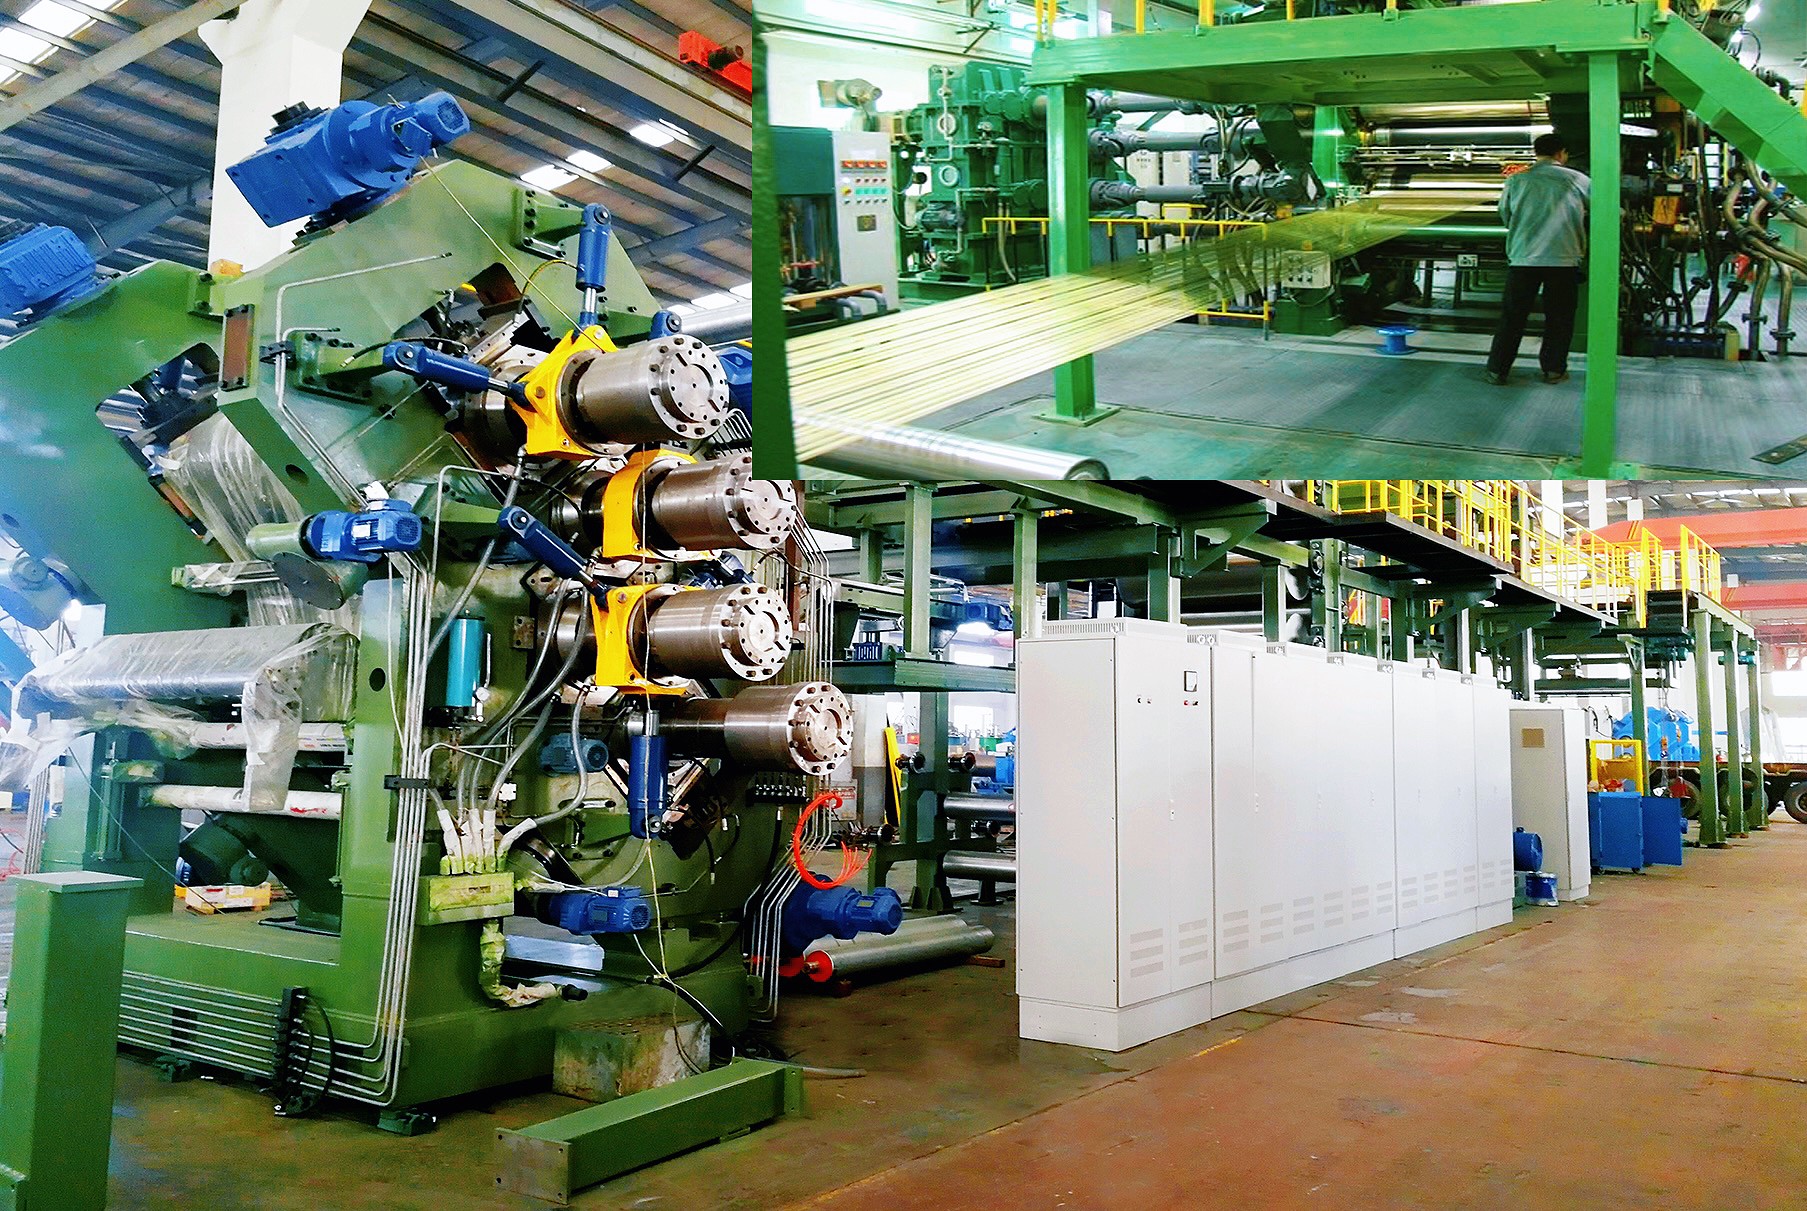
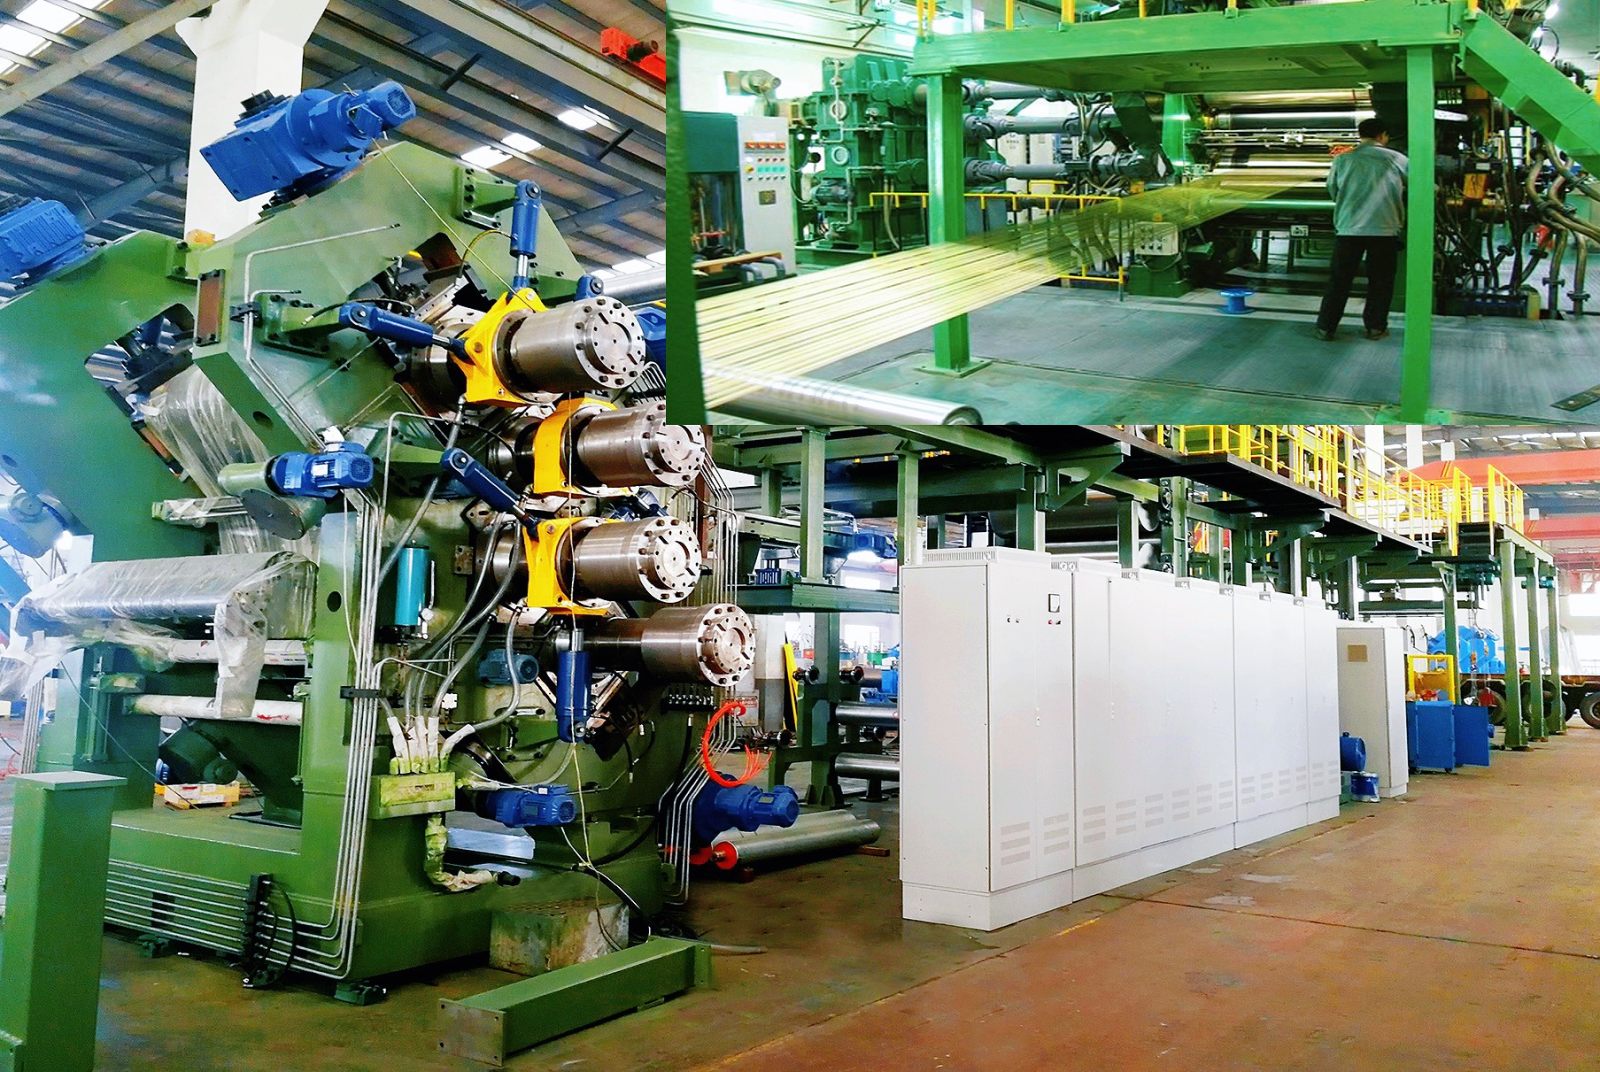
The steel wire cord four-roll calendering production line is dedicated equipment for the core skeleton materials of radial tires. Through hot calendering, it double-side compounds copper-plated steel wire with rubber to produce high-strength, low-stretch steel wire cord fabric; it is used for the production of all-steel radial tire carcasses, belt layers, and other products.
Product features: The main calendering machine adopts four high-strength alloy chilled cast iron/forged alloy steel rolls. The roll surface temperature is regulated by an automatic temperature control system, and the roll spacing is automatically adjusted by a high-precision electric/hydraulic roll gap adjustment system. It is equipped with bearing clearance elimination and crown compensation devices. The production line is equipped with PLC + bus control to achieve highly automated operation.
Product Introduction
The steel wire cord four-roll calendering production line is dedicated equipment for the core skeleton materials of radial tires. Through hot calendering, it double-side compounds copper-plated steel wire with rubber to produce high-strength, low-stretch steel wire cord fabric; it is used for the production of all-steel radial tire carcasses, belt layers, and other products.
Product features: The main calendering machine adopts four high-strength alloy chilled cast iron/forged alloy steel rolls. The roll surface temperature is regulated by an automatic temperature control system, and the roll spacing is automatically adjusted by a high-precision electric/hydraulic roll gap adjustment system. It is equipped with bearing clearance elimination and crown compensation devices. The production line is equipped with PLC + bus control to achieve highly automated operation.
Advantages:
Steel wire: High controllability of unwinding tension and strong tension consistency;
Stable calendering roll temperature, roll gap, and speed, with no defects such as rubber leakage or bubbles;
Uniform thickness and density of the finished product, consistent tension, and a flat, smooth surface without wrinkles.
The steel wire cord calendering production line is a tandem line used for calendering and rubberizing steel wire cord fabric, including a rubber calender and its tandem devices; according to the requirements of the rubberizing operation, it is equipped with tandem devices for continuous rubberizing operations. The main process equipment consists of a creel, a wire arranging stand, a splicer, a warping device, a cooling machine, a fabric accumulator, a haul-off machine, a winder, and other control systems. It is a device that arranges the cords neatly according to the specified density and presses and positions the cords onto the rubber-covered calender rolls. It is mainly composed of two parallel grooved warping rollers and their shifting mechanisms. The groove and spacing dimensions of the warping rollers are determined according to the cord type, specifications, and cord fabric density. The warping rollers are driven to shift by the shifting mechanism through motors, air cylinders, or oil cylinders. When threading or arranging the cords, the warping rollers can be moved away from the calender rolls; after threading or arranging the cords is completed, they can be slightly attached to the calender rolls to precisely limit the cord arrangement position and enter the calendering operation state. The creel is composed of a certain number of spindles arranged and fixed on a frame. Cord bobbins can be placed on the spindles. To keep the tension constant when the cords are unwound, each spindle seat is equipped with a control device that automatically adjusts the cord unwinding tension, usually including friction braking, electromagnetic control, and pneumatic control types.
Parameters
Send An Inquiry
Recommended Products